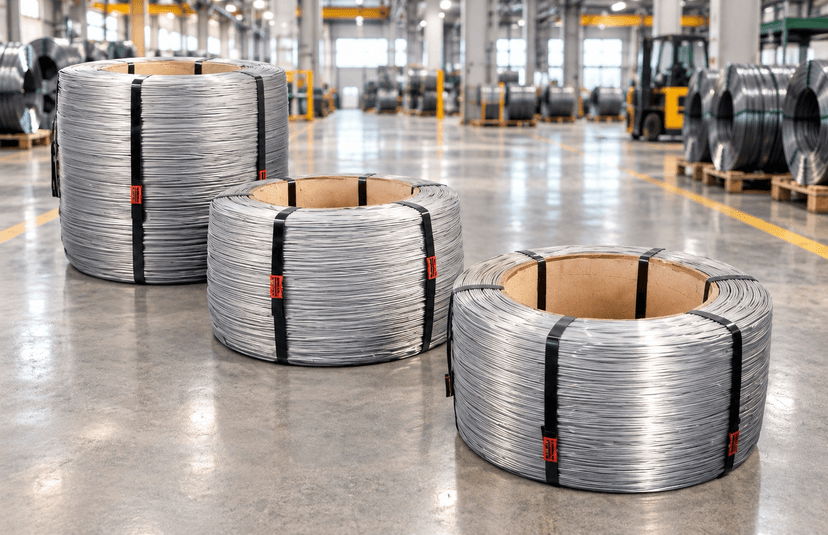
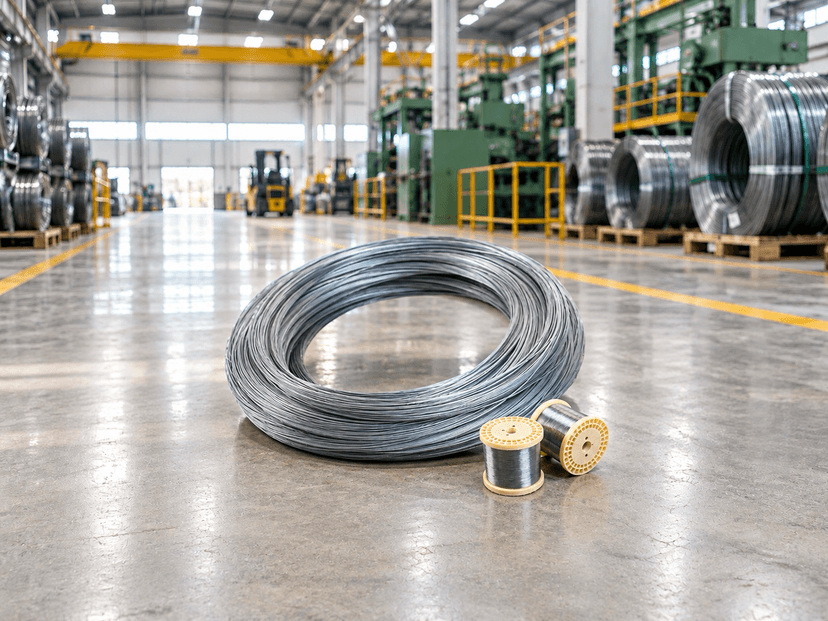
High Carbon Spring Steel Wires
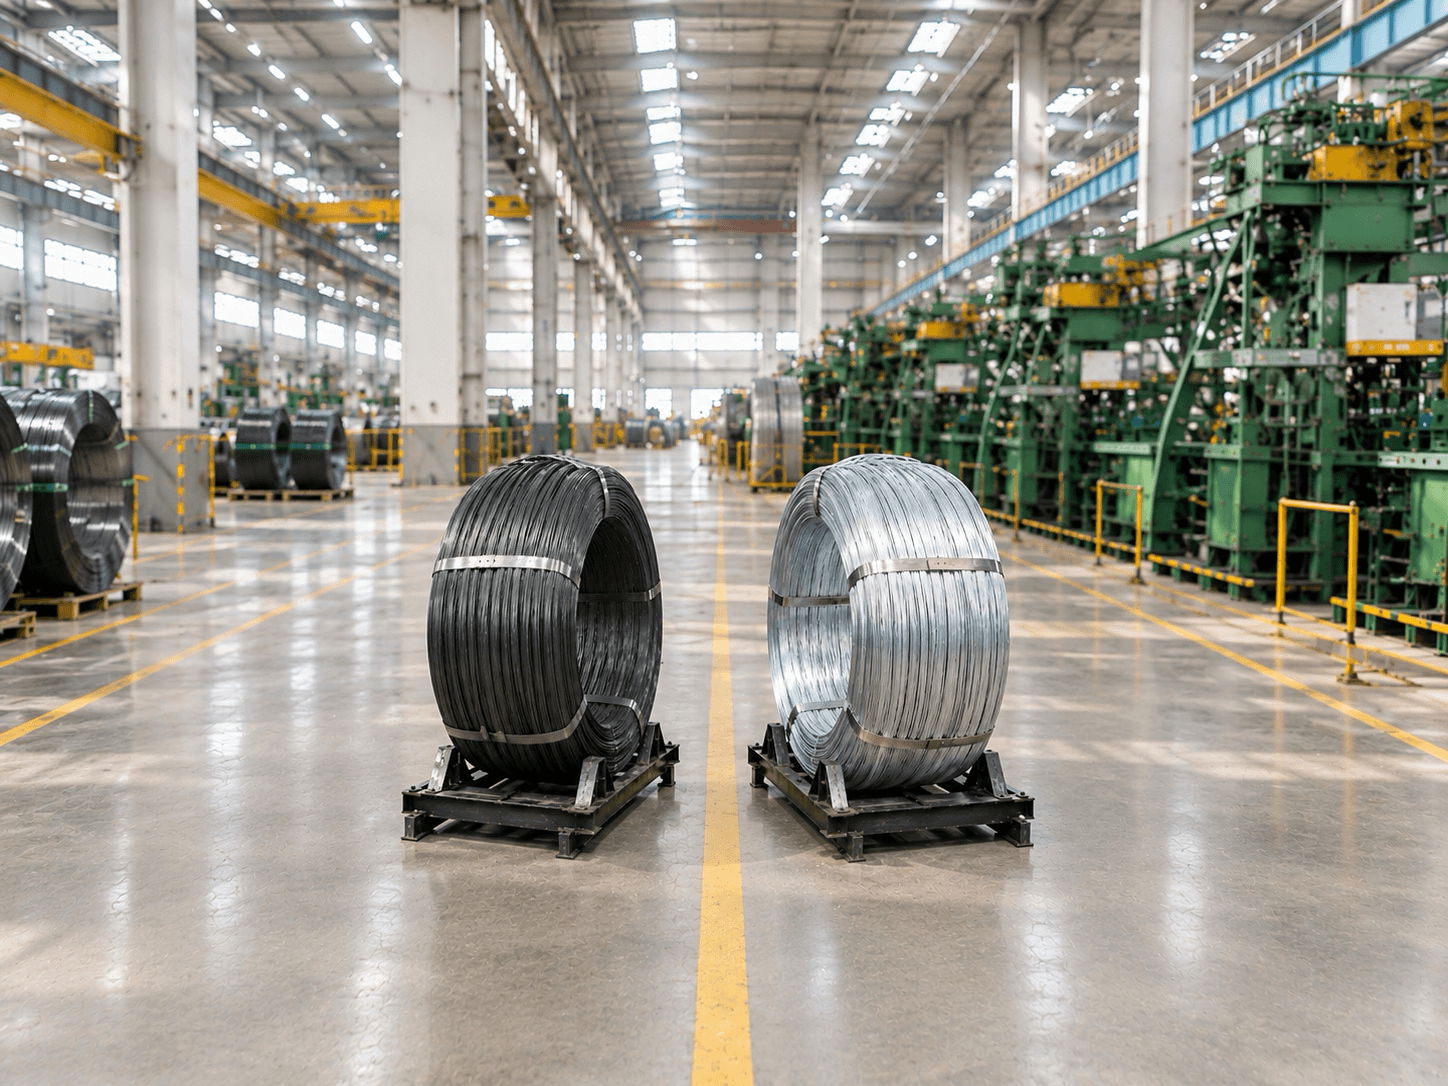
The core line, supplied black, phosphated or galvanized. Four variants sit under it, each held to a different tolerance, temper and finish — dial in the one you need below and the sheet updates with it.
Built around the forming operation,
not just the diameter.
Temper, coating route and tolerance are selected together — which is why the grade you pick changes the tensile band you get.
Five grades, one line
SL, SM, SH, DM and DH supplied off the same line, so the temper is matched to the forming operation instead of the other way round.
Two coating routes
Phosphated where the wire will be drawn and formed; galvanized where the finished part stays exposed. Both run to the same tolerance band.
Held to IS-4454
Every lot lands with dimension, tensile, torsion, wrap, bend and deep-etch results against IS-4454 — or against your specification where it supersedes the standard.
Despatch from three points
Coil, spool and bobbin despatch out of Goregaon, Bhiwandi and Vasai — the nearest unit is assigned at the time of order.
Build the specification you need.
Diameter, grade and finish drive everything downstream — tolerance class, tensile band, coil dimensions and which unit finishes it. Change one and the rest updates.
- Tensile range
- 1 750 – 1 970 N/mm²Indicative for grade & diameter
- Tolerance class
- ± 0.02 mm
- Applicable standard
- IS-4454 Pt 1:2001
- Coil I.D. / O.D.
- 480 / 600 mm
- Coil weight
- 100 – 200 kg
- Packing
- Oiled, polythene wrappedBound at three places minimum
- Dispatch unit
- Assigned at orderGoregaon, Bhiwandi or Vasai
- Wire rod source
- Confirmed on quotation
Your selection is carried into the message — no retyping.
Chemistry, mechanicals
and coil dimensions.
Composition splits by grade group — SL/SM/SH and DM/DH carry different limits, so they are shown apart rather than averaged into one range.
Grades SL, SM, SH
Grades DM, DH
Physical & mechanical properties
Maintained as per IS-4454 Pt 1:2001, or to your drawing where it supersedes the standard.
Held to the band for the selected grade and diameter class, verified per heat before despatch.
Wrapped around a mandrel of specified diameter with no cracking or coating flake-off.
Twist count held to the minimum specified for the diameter class.
Conducted as per IS-4454 Pt 1:2001 or as specified by the customer.
Coiled to the specified index without surface cracking or set.
Surface defects checked by deep etch as per the standard or your specification.
Checked per heat; limits agreed at the time of order where tighter than the standard.
Coil weight & coil dimensionsLive — tracks the diameter set in the selector above
| Wire dia (mm) | Coil I.D. (mm) | Coil O.D. max (mm) | Approx. coil weight (kg) |
|---|---|---|---|
| 0.25 – 0.40 | 130 | 360 | 5 – 15 |
| 0.40 – 0.78 | 160 | 360 | 15 – 25 |
| 0.79 – 1.35 | 280 | 400 | 40 – 80 |
| 1.40 – 2.80 | 480 | 600 | 100 – 200 |
| 2.85 – 4.00 | 630 | 900 | 100 – 200 |
| 4.00 – 8.50 | 750 | 950 | 300 – 500 |
Coils are oiled with rust-preventive oil and packed in polythene or HDPE, or as per your requirement. Spool and coil weights are agreed at the time of order.
High Carbon Spring Steel Wires — technical data sheet
Composition by grade group, mechanical test schedule, tolerance classes, coil dimensions and the full process flow, on two pages.
Three mill routes. Follow yours.
The mill line branches twice: the DD route bypasses descaling, pre-drawing and patenting, and the galvanized route forks after inspection to pick up its own coating and finish-drawing pass. Pick a route and the steps renumber along it.
12 steps
Rolled at the mill, dispatched from our nearest unit
Four ways in.
Pick whichever is quickest.
Every route below carries your selected specification with it, so the first reply can be a price rather than a list of questions.